Certified Personal Protective Equipment & Medical-Grade Facial Protection


Evaluating Material Science Innovations, Supply Chain Optimization, and High-Efficiency Particulate Filtration
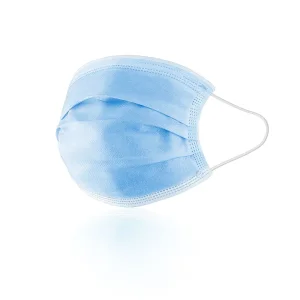
The global demand for high-performance non-woven face masks has transformed from emergency procurement into a highly regulated, quality-driven global supply chain framework. Modern non-woven protective gear relies heavily on complex polymer chemistry—primarily medical-grade Polypropylene (PP)—processed via advanced Spunbond-Meltblown-Spunbond (SMS) and SSMMMS multi-layer composite techniques.
In high-standard clinical and industrial environments, single-layer filtration is insufficient. The critical protective core is the meltblown micro-fibrous matrix, where fibers feature diameters ranging from 1 to 5 micrometers. When treated with high-voltage electrostatic corona charging or hydro-charging, these microscopic webs capture sub-micron airborne particles, bacteria, and viral aerosols via electrostatic attraction, inertial impaction, and Brownian diffusion without sacrificing breathability.
Utilizing virgin homopolymer polypropylene resin with narrow molecular weight distribution, producing continuous filaments engineered for maximum tensile strength and microscopic pore distribution stability.
Inner non-woven layers feature skin-friendly, hypoallergenic thermal-bonded fabrics free of fluorescent agents, latex, or irritating chemical binders, preventing contact dermatitis during prolonged clinical wear.
Fully enclosed dust-free cleanrooms with automated ultrasonic welding, automated earloop fixation, vision-guided deficit checking, and automated unit packaging to guarantee zero human-touch contamination.
Henan Tobe Health Co., Ltd. — A Leader in Integrated Healthcare Technologies & Global Export Infrastructure
Henan Tobe Health Co., Ltd. is a comprehensive medical and health technology enterprise, affiliated with a well-established industrial group. The company integrates research and development, manufacturing, sales, and after-sales service, focusing on protective products, medical devices, medical consumables, and health-related equipment.
The company covers an area of approximately 100 mu, with modern production workshops exceeding 400,000 square meters and a workforce of over 3,000 employees. Its business scope spans multiple sectors including healthcare, medical aesthetics, rehabilitation, and health management services, demonstrating strong industrial integration capabilities.
Driven by a rigorous Quality Management System, Henan Tobe Health operates cleanroom workshops certified to international standards. Combined with continuous capital investment in meltblown technology, high-speed mask forming machinery, and online digital quality monitoring, the factory delivers ultra-consistent barrier performance across millions of units produced daily.
Henan Tobe Health Co., Ltd. has established an advanced R&D center staffed with over 20 experienced engineers and technical experts. The team is dedicated to continuous innovation, product upgrades, and the development of new medical technologies.
The company utilizes state-of-the-art production lines and precision testing equipment, combined with internationally advanced manufacturing management systems. With more than 20 automated mask production lines and diversified equipment manufacturing capabilities, the company ensures stable supply capacity and consistent product quality.
Henan Tobe Health Co., Ltd. operates over 20 automated mask production lines alongside multiple advanced manufacturing lines for medical and health equipment. The company emphasizes efficiency, safety, and quality control throughout the entire production process.
Comprehensive Performance Metrics Across International Standards (ASTM F2100, EN 14683, NIOSH N95, GB2626)
| Classification / Mask Type | Core Standard | BFE / PFE Efficiency | Fluid Resistance | Breathing Resistance (ΔP) | Primary Target Application |
|---|---|---|---|---|---|
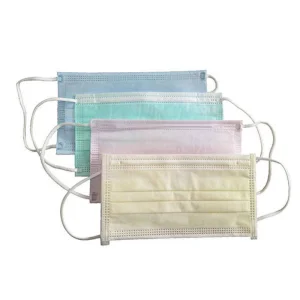
| 3-Ply Surgical Disposable Mask | ASTM F2100 Level 2 / 3 EN 14683 Type IIR |
BFE ≥ 98% PFE ≥ 98% (@ 0.1 μm) |
120 - 160 mmHg | < 5.0 mm H₂O/cm² (< 49.0 Pa/cm²) | Operating Rooms, Clinical Procedure, Hospital Infection Control |
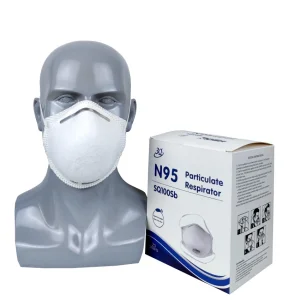
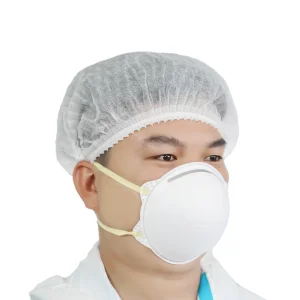
| N95 Particulate Respirator | NIOSH 42 CFR 84 | PFE ≥ 95% (@ 0.3 μm NaCl) | 80 - 160 mmHg | Inhalation ≤ 35 mm H₂O Exhalation ≤ 25 mm H₂O |
High-Risk Aerosol Generating Medical Procedures, Airborne Isolation |
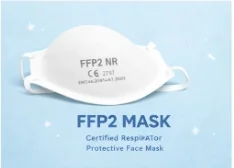
| FFP2 / FFP3 Filtering Facepiece | EN 149:2001 + A1:2009 | FFP2 ≥ 94% FFP3 ≥ 99% (@ 0.6 μm) |
Synthetic Blood Splash Compliant | Inhalation (30L/min) ≤ 0.7 mbar (95L/min) ≤ 2.4 mbar |
Industrial Dust, Mining, Chemical Handling, Pharmaceutical Cleanrooms |
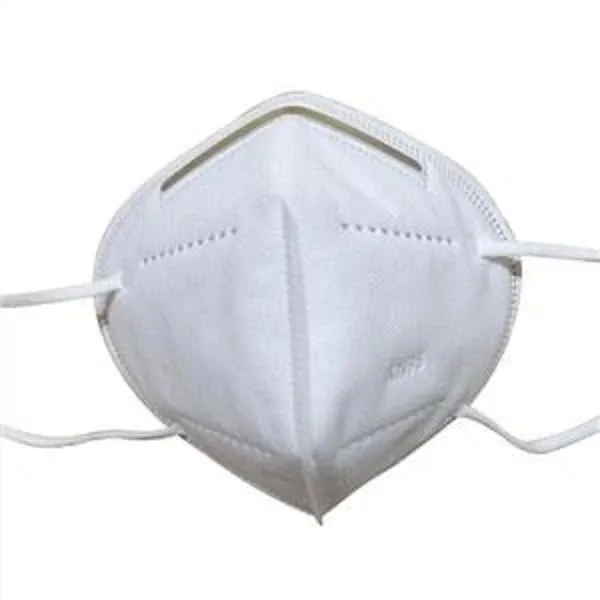
| KN95 Protective Respirator | GB 2626-2006 / GB 2626-2019 | PFE ≥ 95% (@ 0.3 μm) | Splash-Proof Variant Available | Inhalation ≤ 210 Pa Exhalation ≤ 210 Pa |
Civilian Protection, Industrial Fine Dust, Public Health Containment |
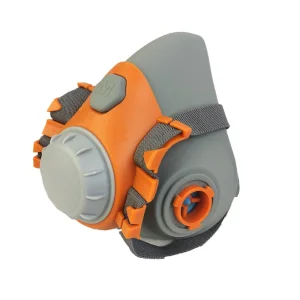
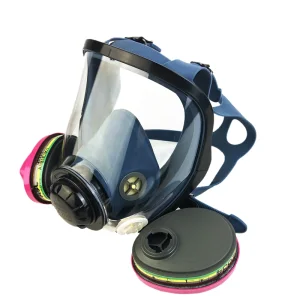
| Elastomeric Half/Full Face Mask | EN 140 / EN 136 / ABEK1P3R | Filter Cartridge P3 ≥ 99.95% | Heavy Chemical Splash Protection | Low Resistance Dual Cartridge System | Heavy Industrial Chemical Gases, Vapors, Toxic Particulates |
Our non-woven masks utilize automated ultrasonic edge sealing to eliminate structural pinholes that cause seal leakage. Soft, highly elastic flat earloops (or headbands) reduce ear pressure by over 40% during long shifts. Embedded aluminum or double-wire plastic nose clips ensure dynamic facial contour sealing.
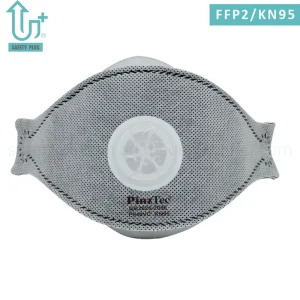
For specialized industrial environments, an extra active carbon non-woven layer is integrated. Carbon web layers absorb organic vapors, nuisance odors, ozone, and toxic gaseous pollutants, delivering combined particulate and gaseous filtration for painting, welding, and chemical processing.
E-E-A-T Compliance Framework: Verified International Standards and Quality Systems
The company strictly adheres to international and domestic quality standards. Its products have obtained multiple authoritative certifications, ensuring seamless entry into North American, European, Asian, and Latin American health sectors:
Ministry of Commerce (MOFCOM) PPE Export Whitelist Listed:
Henan Tobe Health Co., Ltd. is listed on the official PPE export whitelist of the Ministry of Commerce of China, ensuring 100% legal compliance, smooth customs clearance, and global trade credibility.
Comprehensive continuous improvement loop, raw material traceability, online automated optical inspection, and lot-by-lot particle penetration testing.
Eco-friendly clean manufacturing process, solvent-free ultrasonic welding, zero hazardous waste release, and recyclable PP material management.
Ensuring pristine operational standards for 3,000+ employees, ergonomic workstations, and sterile environment controls.
Custom OEM/ODM Engineering Solutions Tailored for Diverse Global Environments
ASTM Level 2/3 and Type IIR masks engineered specifically for operating theaters, emergency rooms, and dental clinics. Features high synthetic blood splash barrier and ultra-soft inner lining to protect surgeons during extended operations.
NIOSH N95, FFP2, and Heavy Duty Silicon Respirators designed for harsh industrial applications including silica dust exposure, mining, metal grinding, wood sanding, and chemical spraying environments.
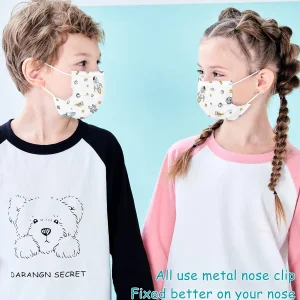
Specially sized KF94 and printed 3-ply masks tailored to child ergonomics. Designed with smaller dead-space volumes, ultra-low breathing resistance, and cute patterns to encourage compliance in schools and public travel.
Next-Generation Non-Woven Filtration Technologies, Biodegradable Materials, and Smart PPE Manufacturing
As the non-woven face mask industry advances, Henan Tobe Health Co., Ltd. is actively expanding its R&D roadmap toward three technological pillars:
Company Philosophy: Customer-oriented, driven by innovation, Henan Tobe Health Co., Ltd. is committed to promoting advanced medical technologies, enhancing end-user service value, and contributing to the global healthcare industry.
Company Vision: To become a leading high-tech enterprise with core technologies and integrated system solutions in the medical and health industry, making significant contributions to the advancement of medical equipment and global health services.
Company Mission: To integrate science and technology into healthcare and improve the quality of human life through innovation and reliability.
Essential Technical, Compliance, and Sourcing Information for Global Distributors & Healthcare Authorities
Since 2020, Henan Tobe Health Co., Ltd. has actively expanded into the global market. Its products have been exported to more than 30 countries and regions, including the United States, Canada, the United Kingdom, Italy, France, Spain, Japan, India, and countries across the Middle East, Africa, and South America.
Through reliable product quality and strong supply capacity, the company has made significant contributions to global public health and epidemic prevention efforts.
The company is supported by a professional international sales and service team, providing:
High-Performance Non-Woven Filtration Masks & Specialty Protective Equipment
 Tobe Health