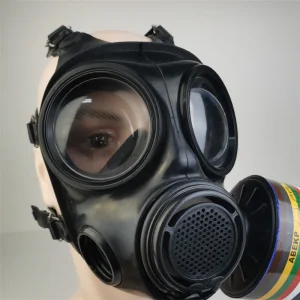
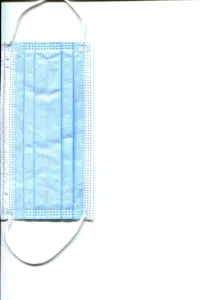
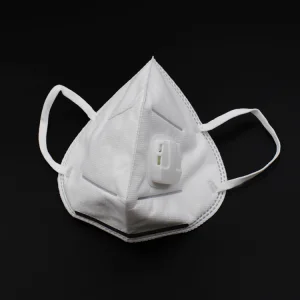
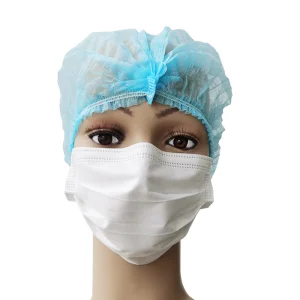
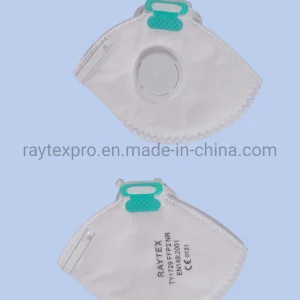
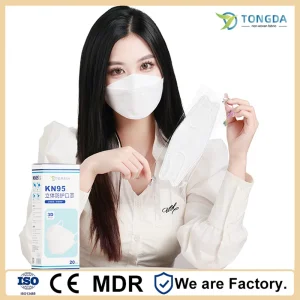
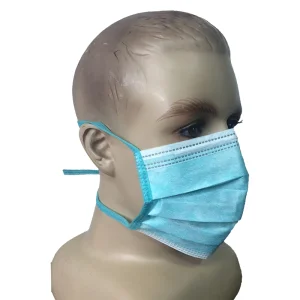
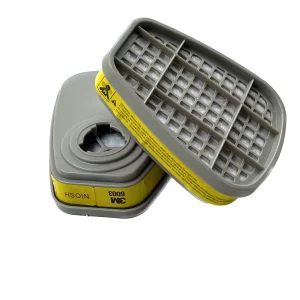
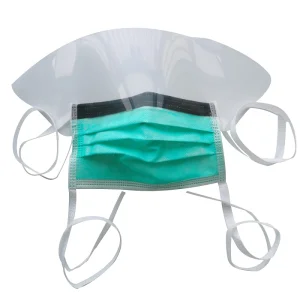
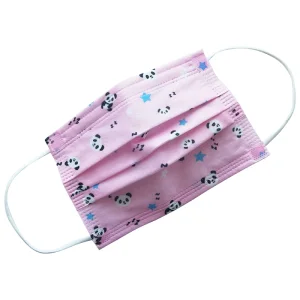
Henan Tobe Health Co., Ltd. is a comprehensive medical and health technology enterprise, affiliated with a well-established industrial group. The company integrates research and development, manufacturing, sales, and after-sales service, focusing on protective products, medical devices, medical consumables, and health-related equipment.
The company covers an area of approximately 100 mu, with modern production workshops exceeding 400,000 square meters and a workforce of over 3,000 employees. Its business scope spans multiple sectors including healthcare, medical aesthetics, rehabilitation, and health management services, demonstrating strong industrial integration capabilities.
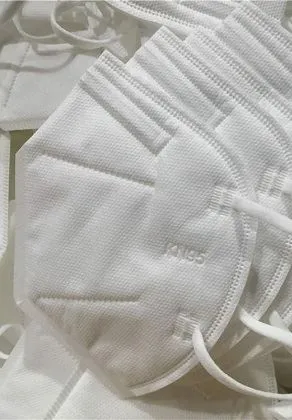
Henan Tobe Health Co., Ltd. has established an advanced R&D center staffed with over 20 experienced engineers and technical experts. The team is dedicated to continuous innovation, product upgrades, and the development of new medical technologies.
The company utilizes state-of-the-art production lines and precision testing equipment, combined with internationally advanced manufacturing management systems. With more than 20 automated mask production lines and diversified equipment manufacturing capabilities, the company ensures stable supply capacity and consistent product quality.
The company strictly adheres to international and domestic quality standards. Its products have obtained multiple authoritative certifications, including:
Additionally, the company has been listed on the PPE export whitelist of the Ministry of Commerce of China, ensuring compliance and credibility in global trade.
Customer-oriented, driven by innovation, Henan Tobe Health Co., Ltd. is committed to promoting advanced medical technologies, enhancing end-user service value, and contributing to the global healthcare industry.
To become a leading high-tech enterprise with core technologies and integrated system solutions in the medical and health industry, making significant contributions to the advancement of medical equipment and global health services.
To integrate science and technology into healthcare and improve the quality of human life through innovation and reliability.
The future of respiratory protection lies in advanced material science. Traditional melt-blown nonwoven fabrics are rapidly evolving toward electrospun nano-fiber matrices. These next-generation filtering media drastically reduce breathing resistance while capturing sub-micron particulate matter, bacteria, and viral aerosols with over 99.9% efficiency.
Furthermore, smart sensory integration is on the horizon. Tobe Health's R&D pipeline includes humidity and pressure sensors embedded within half-face masks and surgical respirators to monitor real-time user fatigue and filter saturation indices in hazardous industrial environments.
As a leader in industrial manufacturing, Tobe Health champions Factory 4.0 standards. By fusing IoT-enabled automated production lines with strict optical computer-vision inspection systems, every single mask undergoes automated defect detection before packaging.
Our macro-solutions support governments, hospital conglomerates, and industrial distributors globally, providing customized B2B bulk manufacturing that guarantees supply chain resilience during global health crises and industrial emergencies.
Global procurement directors require absolute reliability, traceability, and scalable volume. Henan Tobe Health Co., Ltd. addresses these demands through:
Since 2020, the company has actively expanded into the global market. Its products have been exported to more than 30 countries and regions, including the United States, Canada, the United Kingdom, Italy, France, Spain, Japan, India, and countries across the Middle East, Africa, and South America.
Through reliable product quality and strong supply capacity, Henan Tobe Health Co., Ltd. has made significant contributions to global public health and epidemic prevention efforts.
The company is supported by a professional international sales and service team, providing:
Henan Tobe Health Co., Ltd. remains committed to building long-term partnerships with global clients through professionalism, quality, and trust.
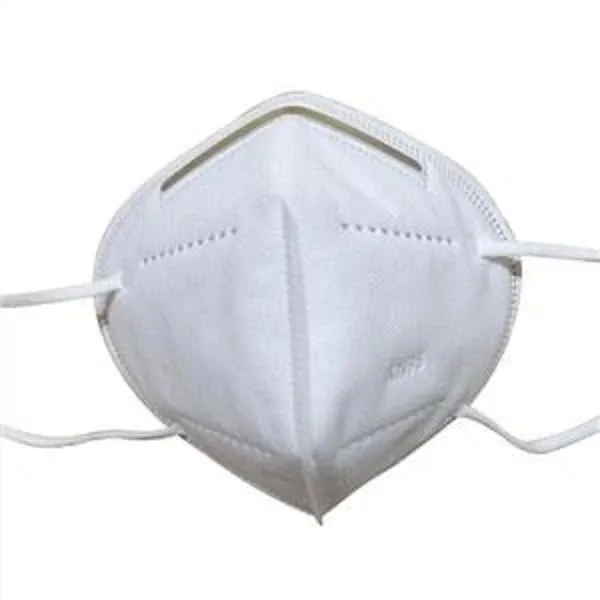
Our masks comply with major global regulatory standards, including EU CE certification, US FDA registration, ISO9001/ISO14001/ISO45001 management systems, and China National Standards such as GB2626 and GB/T32610, ensuring full legal and quality compliance for international trade.
Yes. With over 400,000 square meters of production workshops, 20+ automated manufacturing lines, and a workforce exceeding 3,000 employees, we possess immense scalability to fulfill high-volume OEM/ODM orders with customized packaging, branding, and specification adjustments.
Our products have been successfully exported to over 30 countries and regions worldwide, including the United States, Canada, the United Kingdom, France, Italy, Spain, Japan, India, as well as nations across the Middle East, Africa, and South America.
We integrate strict optical computer-vision inspection systems on our automated production lines alongside precision laboratory testing equipment. Every batch undergoes rigorous filtration efficiency, breathability, and tensile strength testing prior to global shipment.
 Tobe Health