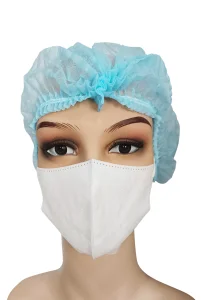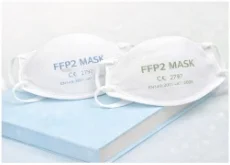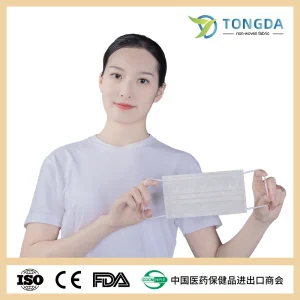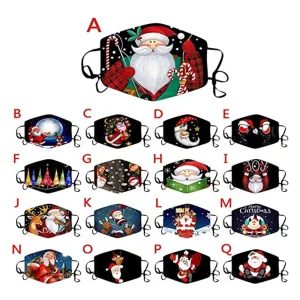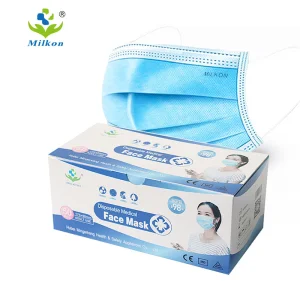
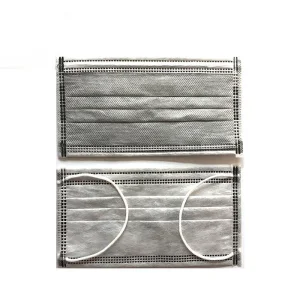
Henan Tobe Health Co., Ltd. is a comprehensive medical and health technology enterprise, affiliated with a well-established industrial group. The company integrates research and development, manufacturing, sales, and after-sales service, focusing on protective products, medical devices, medical consumables, and health-related equipment.
The company covers an area of approximately 100 mu, with modern production workshops exceeding 400,000 square meters and a workforce of over 3,000 employees. Its business scope spans multiple sectors including healthcare, medical aesthetics, rehabilitation, and health management services, demonstrating strong industrial integration capabilities.
In today's complex industrial and healthcare environments, international enterprise sourcing managers demand stringent validation, scalability, and regulatory compliance. As a premier CE Certified Dust Respirator Manufacturer & Exporter, Henan Tobe Health bridges the gap between massive volume capacity and uncompromised filtration safety.
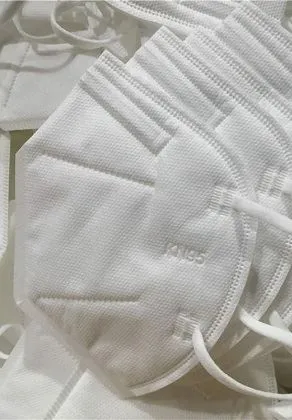
Heavy manufacturing, construction, mining, and chemical processing require heavy-duty dust respirators (FFP2, FFP3, N95 equivalents) capable of blocking micro-particulates, silica dust, and toxic aerosols in compliance with occupational health directives.
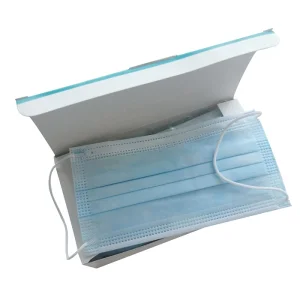
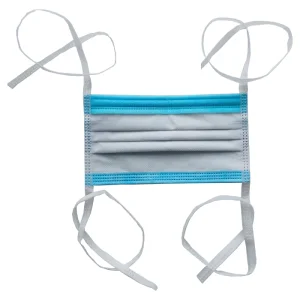
Hospitals and clinics require fluid-resistant surgical masks and medical-grade respirators meeting EN14683 Type IIR and ASTM F2100 Level 3 standards to protect practitioners during critical operations and airborne infection isolation procedures.
Global buyers prioritize tier-one manufacturing partners who maintain redundant automated production lines, stable raw material pipelines, and robust logistics infrastructure to prevent supply disruptions during global health emergencies.
Our portfolio is meticulously engineered to address diverse consumer and industrial requirements. Backed by an advanced R&D center featuring over 20 veteran engineers, we continuously elevate filtration efficiency and ergonomic comfort.
Utilizing state-of-the-art production lines and precision testing equipment combined with international manufacturing management systems, we operate more than 20 automated mask manufacturing lines. This guarantees uncompromised lot-to-lot consistency, superior breathability, and absolute barrier protection.
Trust in global procurement is built upon verified compliance. Henan Tobe Health strictly adheres to rigorous international and domestic regulatory benchmarks, securing full accreditation across major global markets:
EU CE Certification, EN14683, and EN149 compliance ensuring full market access across the European Economic Area.
US FDA Registration and Emergency Use Authorization (EUA) alignment for institutional healthcare procurement.
ISO9001 (Quality), ISO14001 (Environmental), and ISO45001 (Occupational Health & Safety) certifications.
Additionally, our inclusion on the official PPE export whitelist of the Ministry of Commerce of China guarantees absolute trade credibility and customs clearance efficiency worldwide.
Since 2020, Henan Tobe Health has expanded its footprint aggressively into international markets. Our premium protective respirators and masks are exported to more than 30 countries and regions, including the United States, Canada, the United Kingdom, Italy, France, Spain, Japan, India, and key hubs across the Middle East, Africa, and South America.
Supported by an expert international sales and logistics team, we deliver comprehensive client support:
 Tobe Health